Reading Time | 10 Minutes
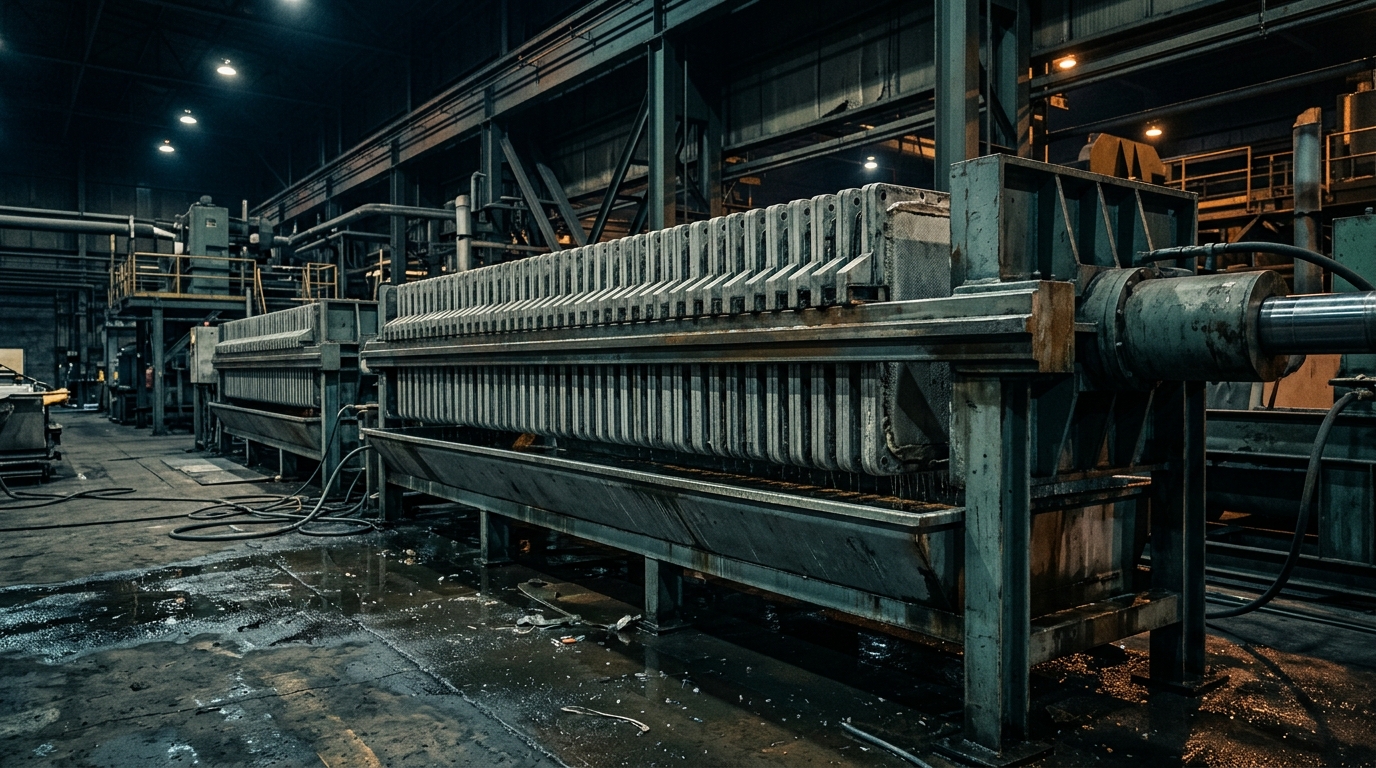
Walking your filter press area tells you a lot: cake condition, cloth appearance, whether filtrate is running clear. But a visual walkthrough isn’t a performance baseline.
Without measured numbers, decline is invisible until it shows up on an invoice. In one case from our hauling-cost analysis, monthly hauling climbed from about $8,000 to roughly $13,000 as cakes got wetter. Nobody on the floor could point to the day it started. A filter press performance baseline is how you see that day coming.
A filter press performance baseline is a set of measured values (feed solids, cycle time, cake solids, filtrate quality, and polymer consumption) recorded over a run of normal cycles when the press is known to be working well. It becomes the reference point that makes drift visible, so you can act before wet cakes and long cycles raise operating costs.
Most facilities don’t have one. Operators know what normal looks like, but they can’t tell you what normal measures, or whether the press is running at 85% of what it should or 60%.
Five core parameters give you a complete picture, and three supporting ones help explain changes when they happen:
| Parameter | How to measure | Unit | Drift that matters |
|---|---|---|---|
| Feed solids | Grab sample from the feed line each cycle; oven-dry | % total solids | Shifts that explain changes in cycle time or dose |
| Cycle time | Feed start to cake discharge, logged per cycle | minutes | Rising while feed solids hold steady |
| Cake solids | Composite sample from top, middle, and bottom chambers; oven-dry | % dry solids | Falling below your dialed-in number |
| Filtrate quality | Sample after the first few minutes of feed | TSS (mg/L) or turbidity (NTU) | Persistent cloudiness after the cake forms |
| Polymer consumption | Active polymer used ÷ dry solids processed | lb per dry ton | Rising without better cake solids |
| Terminal feed pressure (supporting) | Pressure and time to reach it, from the feed pump gauge | psi / minutes | Taking longer to reach pressure |
| Cloth wash interval (supporting) | Cycles between cloth washes | cycles | Washes needed more often |
| Throughput (supporting) | Dry solids per cycle or per day | dry tons | Falling at the same operating hours |
Feed solids is the context for every other number. A longer cycle on a day when feed solids jumped is expected. A longer cycle on a normal-feed day is a problem. If your feed varies a lot by shift or product, see how sludge variability throws off your filter press.
Cycle time is your primary diagnostic. Log it in minutes from feed start to cake discharge. When cycle time increases without a change in feed solids, something is wrong: conditioning drift, cloth blinding, or a feed pump that’s no longer reaching pressure. In the hauling-cost case, re-optimizing the program brought cycles from 95 minutes back to 74.
Cake solids, expressed as percent dry weight, tells you how well the press is dewatering. Wetter cake means you’re paying to haul water. There’s no universal target, because achievable cake solids depend heavily on what you’re dewatering:
| Solids type | Reported cake solids | Source |
|---|---|---|
| Municipal primary + waste activated sludge | 35–50% | U.S. EPA fact sheet (recessed plate presses) |
| Metal hydroxide (metal finishing) | About 25% up to 50–65%, depending on chemistry and press | Micronics |
| Mineral fines (stone, concrete, aggregate) | 62% → 72% in one optimized system | ChemREADY hauling-cost case |
What matters most is the number your press achieves when it’s dialed in. Treat that as the floor. Pull samples from several chambers, because cake is usually wetter at the center and the bottom of a chamber than at the edges.
Measure filtrate; don’t just look at it. Filtrate often runs cloudy for the first few minutes of a cycle, until a cake layer forms on the cloth, so sample after that point. Persistently turbid filtrate points to poorly conditioned solids (fines passing through), a torn cloth, or a leaking plate seal.
Blinding usually shows up as slow, not cloudy. A blinded cloth restricts flow, so you see longer cycles, slower pressure build, and wetter cakes, often with clear filtrate. Cloudy filtrate is usually a conditioning or cloth-damage problem. Mixing the two up sends you to the wrong fix.
Track active flocculant used per dry ton of solids processed. This connects dewatering performance directly to operating cost. If consumption climbs without better cake solids, the program needs evaluation, and jar testing will tell you whether you’re at the right dose for current feed conditions. Some programs also use a coagulant; track it the same way.
Once you know what to measure, the next question is how much data makes a baseline.
Log all parameters across 10–15 consecutive full cycles under normal operating conditions. Exclude cycles during maintenance, startup after a shutdown, or periods when feed chemistry changed. The goal is to capture what normal actually produces, so deviations are obvious when they happen. Follow these six steps:
What we usually find on a first baseline. Something was already moving: cycle times trending up over six months, cake solids two to four points below what the system can achieve, or polymer dose set higher than current feed conditions need.
We run jar tests, cloth and pressure checks, and cycle studies to find what your press should produce, then build the baseline with your team.
Explore Dewatering Optimization →When a parameter moves 10% or more from baseline in either direction, treat it as a signal, not an anomaly. Use this table to decide where to look first:
| What changed | Likely causes | Check first |
|---|---|---|
| Cycle time up, feed solids steady | Conditioning drift, cloth blinding, feed pump not reaching pressure | Jar test; cloth condition; time to terminal pressure |
| Cake solids down | Under- or over-dosed polymer, short cycle, low terminal pressure | Polymer dose vs. jar test; pressure log |
| Filtrate turbid after cake forms | Poor conditioning, torn cloth, leaking plate seal | Jar test; cloth and gasket inspection |
| Polymer per dry ton up, cake unchanged | Overdosing, feed chemistry change, makedown problem | Jar test; polymer makedown and metering |
| Cloth washes needed more often | Blinding from fines, scale, or excess polymer | Cloth inspection; wash method and frequency |
Many of these trace back to how polymer is made down and dosed. Automated metering, like a Bifloc flocculant metering system, holds dose steady as feed changes. Dewatering monitoring technology can log cycle data automatically, so the baseline updates itself. When a cause turns out to be mechanical, our maintenance and support team can help.
A baseline turns slow decline into a number you can act on. In the hauling-cost case, catching and correcting drift cut hauling by about 37%, from roughly $13,000 to $8,200 a month, and lowered polymer cost per ton at the same time. The work paid for itself in under three weeks. You can estimate your own numbers with our filter press and dewatering ROI calculators.
The baseline doesn’t replace the walkthrough. It completes it. The walkthrough tells you what you’re seeing; the baseline tells you what it measures. Together, visual checks and measured data are a filter press program, whether you run a Matec filter press you own or a rental press on a project.
ChemREADY offers a free on-site analysis. We'll walk your press area, test your feed and filtrate, and give you a plain-English report on what your press should be producing. No obligation.
Schedule Your Free Analysis →It depends on what you are dewatering. The U.S. EPA reports roughly 35 to 50 percent cake solids for municipal primary and waste activated sludge on recessed plate presses, while metal hydroxide cakes range from about 25 percent to 50 to 65 percent, and mineral fines such as stone or concrete slurry can reach about 70 percent. The best benchmark is what your own press achieves when it is dialed in.
Measure cycle time in minutes from the start of feed to the end of cake discharge, and log it for every cycle. Record feed solids alongside it, because cycle time naturally rises when feed solids increase. A rising cycle time with steady feed solids signals conditioning drift, cloth blinding, or a feed pump problem.
Filtrate is often cloudy for the first few minutes of a cycle until a cake layer forms on the cloth. Persistent cloudiness after that usually points to poorly conditioned solids, a torn filter cloth, or a leaking plate seal. Cloth blinding typically causes slow cycles and wetter cakes rather than cloudy filtrate.
Divide the pounds of active polymer used over a period by the dry tons of solids processed in the same period. Dry tons come from cake weight multiplied by cake solids percentage. Tracking this ratio connects dewatering performance directly to chemical cost.
Review your baseline monthly and rebuild it after any major change, such as new filter cloths, a polymer switch, a new product line, or an upstream process change. If your feed varies by season or product, keep a separate baseline for each condition.
A ChemREADY dewatering specialist can run the jar tests and cycle study with your team and set the numbers your operators should track.
Talk to a Specialist →Or call 800-229-6801
Jar-tested flocculant programs matched to your feed, so polymer per dry ton stays where it should.
Explore flocculants →Cloth, plate, and feed pump service to keep cycle times and cake solids at baseline.
Explore maintenance & support →Stone Cutting · Concrete Slurry · Aggregates · Mining · Industrial Wastewater